
BEST FIT
Choose B58 if:
- The machine needs a coordinated fourth axis.
- Color-screen path preview is useful for the rotary workflow.
- The rotary drive, CAM output and supplied interface can be matched.

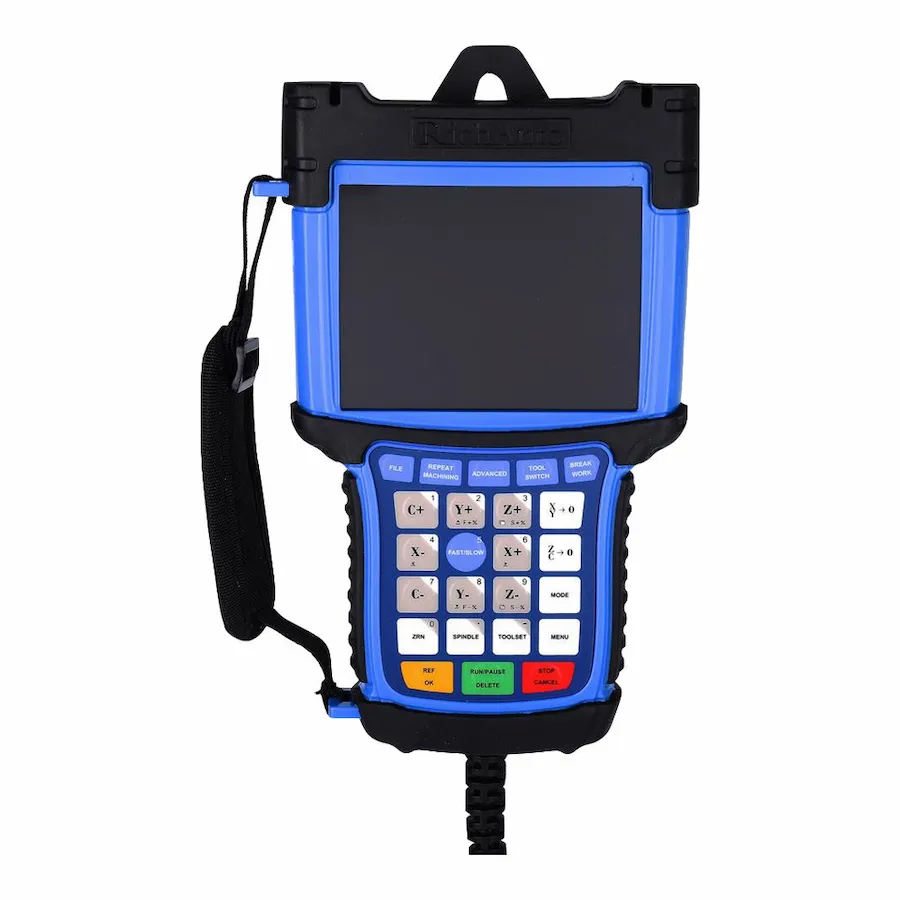
RichAuto B58 handheld front panel and color display. Reference photo; confirm the supplied controller and interface-board revision.
B5X SERIES · RA-B58
Four-axis DSP control with a color display for rotary carving and machining that needs a coordinated fourth axis.
Series: Browse the B5X controller range
CINKR supplies new, genuine RichAuto controllers and supports single-unit replacement orders. Eligible faults are covered by a one-year warranty. Most orders are dispatched within three working days after payment.
The supplied components, configuration, shipping cost and delivery estimate are confirmed in your quotation. Delivery, warranty and return terms.
PRODUCT GUIDE
Four-axis B5X DSP control for rotary carving and multi-axis machining, featuring 5-inch color display, dynamic graphical preview and 4.0 MHz pulse rates.
QUICK DECISION
BEST FIT
CHECK BEFORE ORDERING
CONSIDER ANOTHER MODEL IF
The RichAuto B58 represents the flagship four-axis standalone DSP motion control architecture engineered for high-precision rotary carving machines, 3D architectural column shapers, and multi-axis CNC machining centers. Designed for demanding industrial environments, the B58 pairs four fully synchronized motion channels (X, Y, Z, and A/C) with a high-resolution 5-inch color graphical LCD display, high-speed 4.0 MHz differential pulse generation, and industrial TCP/IP Ethernet networking.
From continuous 3D contouring of intricate stone statues and wooden balusters to multi-sided rotation of mechanical parts, the B58 delivers smooth coordinate interpolation without the software crashes and latency common to PC-based controllers. Operators can simulate rotary toolpaths visually on the color screen, verify coordinate limits, and manage production routines via an ergonomic handheld pendant. Machine builders and retrofitters can request a B58 quote configured for their exact rotary drive specifications.
Four-axis CNC machining centers feature controller tags designated B58, B58E, B58S, or B58C:
| Model Marking | Keypad Faceplate Language |
|---|---|
| B58 | Base 4-axis B5X motion platform |
| B58E | English-only keypad faceplate (Export standard) |
| B58S | Bilingual (Chinese + English) keypad faceplate |
| B58C | Bilingual (Chinese + English) keypad faceplate |
All four-axis simultaneous rotary interpolation, 3D toolpath simulation, 4.0 MHz differential pulse generation, and firmware are identical across B58, B58E, B58S, and B58C. The only difference is the button faceplate language. Choosing between B58E and B58S depends entirely on operator language preference. Confirm whether your axis drives require standard or B58E-1 servo interface boards, then request a B58 specification review.
Standard RichAuto B58 four-axis control packages arrive equipped with industrial hardware for cabinet integration:
Verify all terminal screw blocks and ribbon connectors for mechanical integrity prior to cabinet commissioning.
The B58 provides flexible kinematic settings matching diverse machine architectures:
Verify your CAM post-processor angular output formatting prior to setting machine work zero coordinates, or request a B58 specification review.
Field connections terminate at the B5X four-axis interface breakout board. Engineering documentation identifies two primary hardware revisions:
| Terminal Group | Terminal Identification | Controlled Signal | Electrical Specification |
|---|---|---|---|
| Axis Motion Outputs | PUL+, PUL-, DIR+, DIR- (X, Y, Z, A) | Differential step and direction lines | 5V RS-422 differential, 4.0 MHz max |
| Logic Power Input | 24V+, GND | Primary board DC logic supply | 24V DC regulated, 2A isolated supply |
| Digital Inputs (1-16) | IN01 through IN16 | Homing, limits, tool setting touch plate | Optically isolated 24V NPN sinking inputs |
| Digital Outputs (1-16) | OUT01 through OUT16 | Spindle run, multi-speed, coolant | 24V open-collector transistor outputs |
| Handwheel Interface | MPG Port Terminals | Manual pulse generator connection | 5V differential encoder inputs |
Always inspect the physical silkscreen code on your breakout board before completing electrical cabinet connections.
High-precision rotary carving demands precise calculation of rotational pulse parameters:
Pulse Equivalent = (Motor Steps * Drive Microsteps * Gear Ratio) / 360. When driving a 50:1 harmonic gearhead with a 10,000 count/rev AC servo motor, calculate: (10000 * 50) / 360 = 1388.8888 pulses per degree.Applying these calibration measures prevents spiral tool marks and step variances across complex 3D carvings.
Achieving crisp detail on complex four-axis turnings requires precise synchronization between linear gantry motion and rotary chuck rotation:
Careful drive loop tuning ensures that rotational surface speeds harmonize seamlessly with gantry linear feedrates.
Diagnostic alerts on the 5-inch color display assist operators and technicians in isolating operational faults:
| Screen Diagnostic | Underlying Machine Condition | Inspection Procedure |
|---|---|---|
| A-Axis Limit Overrun | Commanded rotary toolpath exceeds programmed software travel | Check program angular bounds; jog axis manually away from limit |
| Servo Drive Trip (X/Y/Z/A) | Motor drive signaled an internal overcurrent or tracking fault | Inspect servo drive front-panel error code; check mechanical binding |
| Spindle Inverter Fault | Spindle drive error contact signaled to controller | Read inverter display panel error code; verify cooling water flow |
| Emergency Stop Active | E-stop button depressed or safety interlock loop broken | Verify 24V continuity through normally-closed safety pushbuttons |
| Encoder Loss / Tracking Trip | Loose encoder feedback cable on servo drive | Inspect servo encoder harness shield and connector lock |
Reviewing servo drive alarm registers and safety circuit continuity resolves the vast majority of operational interruptions.
When ordering a replacement B58 controller, provide our technical engineering desk with the following specifications:
Submit your machine information through our B58 quotation desk for engineering review.
For facilities evaluating multi-axis control packages:
SELECTION CHECKLIST
SPECIFICATIONS
Compare the current B5X platform below. For an existing machine, match the controller label, interface board and software version; reference documents and photos may show earlier hardware.
| Product model | B58 |
|---|---|
| Series | B5X |
| CPU | DSP |
| Internal memory | Ask CINKR for the memory capacity of the supplied controller. |
| Display | 5-inch |
| Communication | USB / TCP/IP |
| Controlled axes | 4 axes |
| Control signal | Differential |
| Drive system | Stepper / Servo — Match the supplied hardware and software version. |
| Inputs | 16 inputs |
| Outputs | 16 outputs |
| Additional I/O | Confirm the board variant and available terminals for additional I/O. |
| Minimum input unit | 0.001 mm |
| Max. pulse frequency | 4 MHz |
| Power supply | 24V DC — Interface-board input; check its rating separately from the handle supply. |
| Interpolation | Line / Arc / Curve — Match the supplied hardware and software version. |
| Breakpoint resume | Supported — Match the supplied hardware and software version. |
| Power-failure recovery | Supported — Match the supplied hardware and software version. |
| Soft / hard limit | Supported — Match the supplied hardware and software version. |
| Password protection | Supported — Match the supplied hardware and software version. |
| Rotary axis | Supported |
| ATC support | Not supported |
| Multi-spindle / cylinders | Not supported |
| Plasma control | Not supported |
| Handwheel / MPG | Supported |
| Network communication | Supported — Match the supplied network interface and transfer workflow. |
COMPARE RELATED CONTROLLERS
Compare current platform applications, axes, display and I/O. Match the supplied board before replacement; earlier hardware may differ.
| Model | Main use | Axes | Display | I/O | Relationship |
|---|---|---|---|---|---|
| B58 | Four-axis rotary machining with color preview | 4-axis | 5-inch | 16 inputs / 16 outputs | Selected model |
| A18 | Four-axis rotary carving | Confirm configuration | 3-inch | 8 inputs / 8 outputs | Same-class option — compare functions, wiring and signals. |
| B18 | Four-axis rotary machining | 4-axis | 4.3-inch | 16 inputs / 16 outputs | Same-class option — compare functions, wiring and signals. |
| B51 | Three-axis routing with color preview | 3-axis | 5-inch | 16 inputs / 16 outputs | Different platform — not a direct replacement. Machine-level compatibility check required. |
B58 alternatives depend on the required motion and machine functions. A related model is not a promise of interchangeable wiring or firmware.
DOWNLOADS
Download reference documents below. Match the controller and interface-board revision before using any wiring instructions. For a replacement or new order, request the documents for the exact supplied hardware from CINKR.
Reference instructions and parameter guidance, mainly in English with some Chinese labels. These reference editions may describe earlier hardware; the supplied unit must match the document.
Free direct downloadReference wiring diagrams with English labels and signal notation. Confirm the matching board revision before using them.
Request the matching files for your hardware revision.Reference wiring diagrams with English labels and signal notation. Confirm the matching board revision before using them.
Request the matching files for your hardware revision.FAQ
The B58 serves as the flagship 4-axis platform, integrating an expansive 5-inch color LCD display with dynamic rotary toolpath simulation, a high-speed 4.0 MHz differential pulse generator, standard TCP/IP Ethernet networking, and two specialized breakout board revisions supporting high-power industrial AC servo drives.
Yes. The fourth axis can be designated as an A-axis (rotating parallel to X), a B-axis (parallel to Y), or a C-axis (rotating parallel to Z), supporting rotary turners, rotational trunnion tables, and swiveling head arrangements.
The B58E standard breakout board provides conventional terminal screw connections for stepper and hybrid systems, while the B58E-1 revision features dedicated multi-conductor servo connectors and isolated servo alarm feedback loops.
Yes. The 5-inch color display renders both linear gantry paths and rotary movements, allowing operators to visually confirm boundary limits, safe retract heights, and rotary zero alignment prior to starting spindle rotation.
Yes. The 5-inch color screen renders dynamic 3D rotational toolpaths, allowing operators to verify rotary retract clearances prior to cutting.
B58E utilizes standard industrial terminal blocks, while B58E-1 features dedicated multi-conductor servo connectors and isolated drive alarm feedback channels.
Both use identical mathematical formulas based on motor steps and gear reduction, but the B58 supports pulse frequencies up to 4.0 MHz, allowing higher rotary rapid traverse speeds.
REQUEST A QUOTE
Tell us the quantity and destination country. For a replacement or upgrade, include any available machine details below. This form only prepares your message; nothing is submitted or stored.