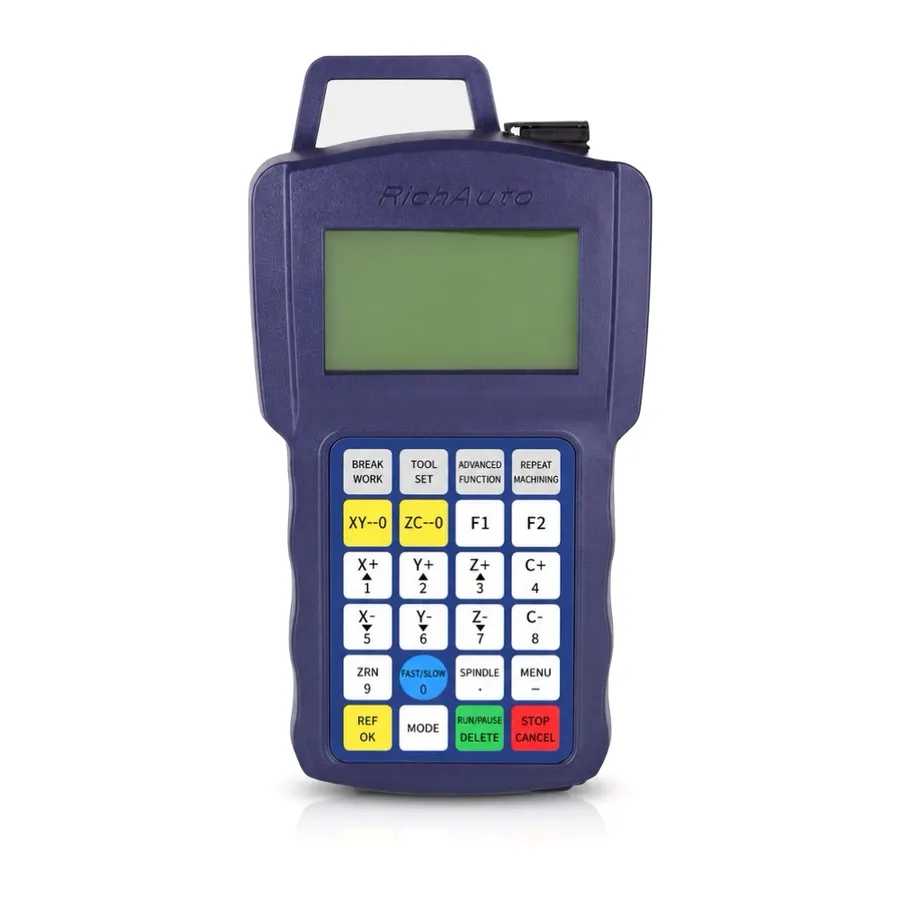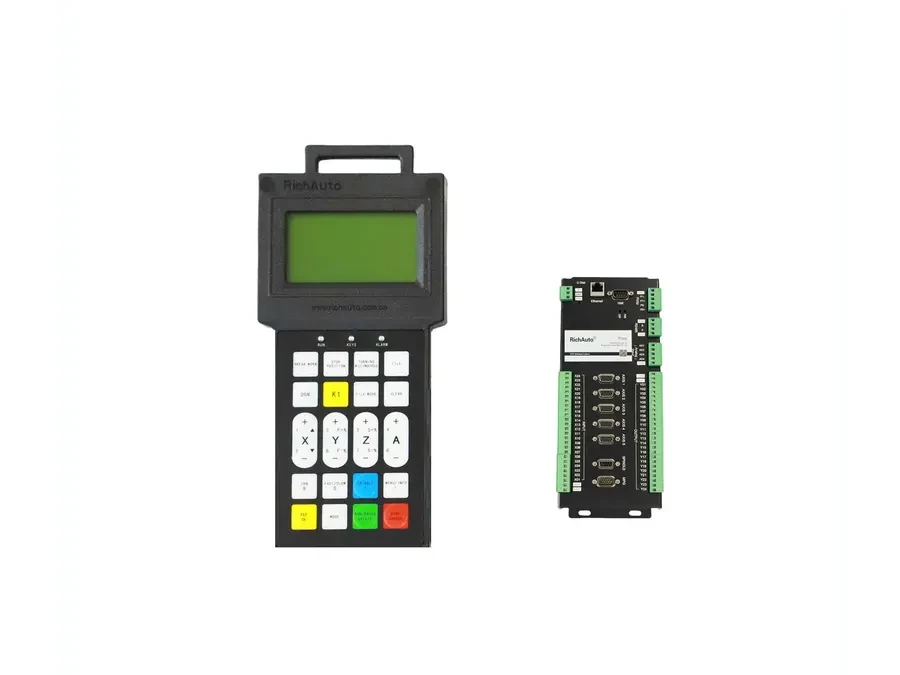
The RichAuto F1410 is intended for stone-processing machines where CNC motion control and surface dotting are part of one workflow. It is relevant when the machine needs three- or four-axis motion, a 24I/24O interface board and the ability to retain dot information without adding a separate dotting device. The machine configuration still determines whether the controller is the right fit.
Define the Stone Workflow First
Identify the workpiece, the engraving or marking process, and how the machine uses surface dotting. Record whether the existing system uses a separate device, how the measured or recorded surface points are handled, and which machine functions must remain available after replacement.
The F1410 is not a general recommendation for ordinary routing, ATC or plasma machines. A model should be selected from the process it must control, not only from a similar DSP format or axis count.
Confirm Three- or Four-Axis Motion
The controller can operate in three-axis or four-axis motion modes. If the machine has a fourth axis, confirm whether it is a normal motion axis or a rotary axis and record the designation used by the machine. The axis count must be reviewed together with the installed drives, I/O and machine workflow.
Check the Electrical Interface
For a new machine, define the required inputs, outputs, drive signals, operator controls and dotting workflow before the cabinet is finalized. For a replacement, photograph the current controller, interface board, terminal labels, drive connections and cabinet wiring before removing anything. Include the controller label and any available parameter records.
Matching the number of axes does not prove that another controller uses the same I/O assignments, interface board or auxiliary signals. This is especially important for older stone machines that may have been modified after installation.
When to Request a Compatibility Review
Request a review when the stone workflow, axis arrangement, board type, drive signals or dotting process is unclear. Send the collected machine information to CINKR before quotation so the intended F1410 configuration can be assessed against the actual machine.