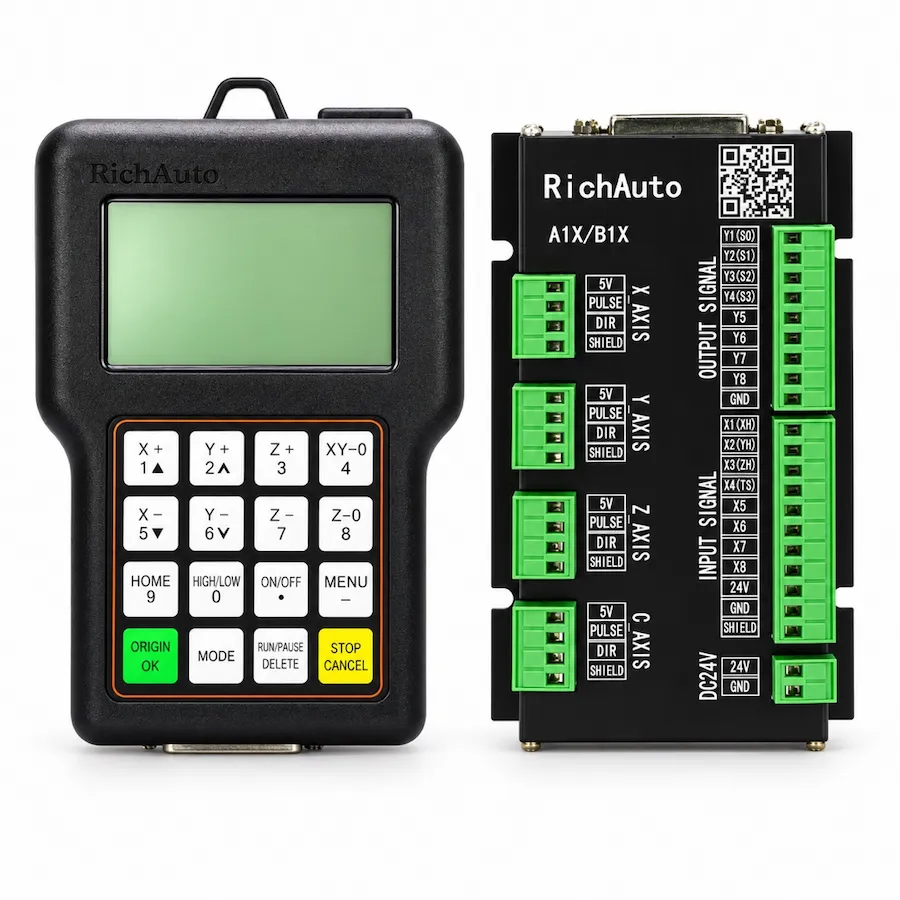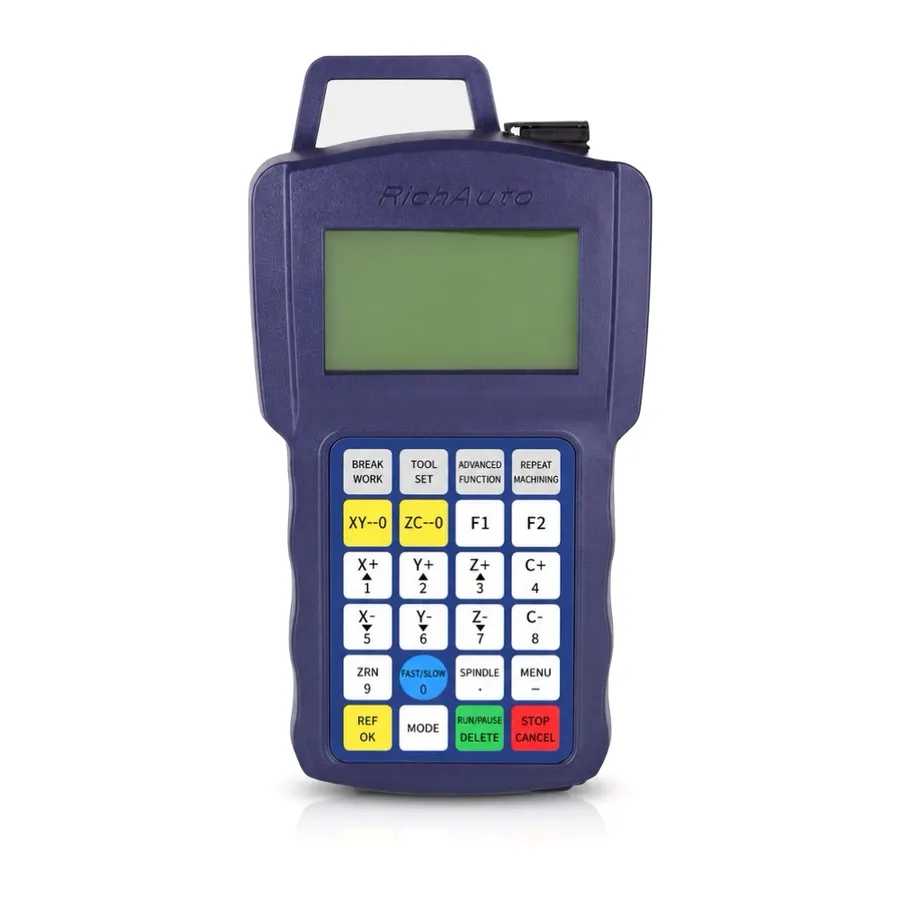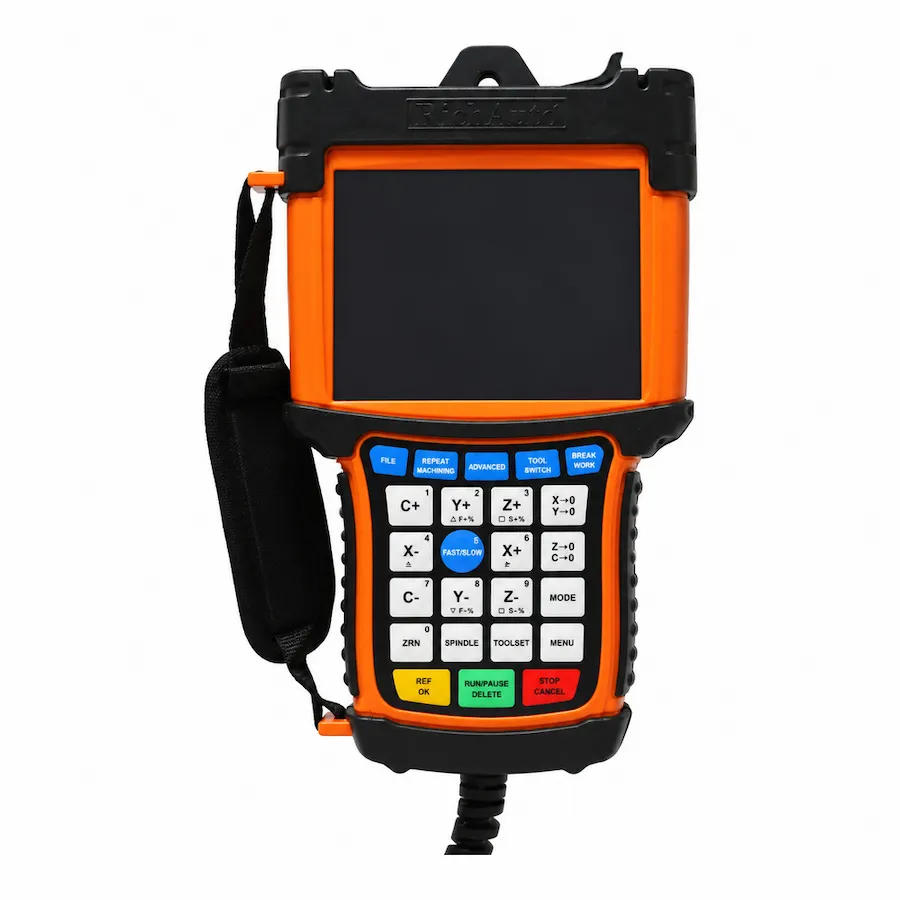
The RichAuto A132 is a CNC lathe and turning controller for machines whose core workflow is X/Z motion rather than a standard router configuration. It can also be relevant to turning-and-engraving equipment or a lathe with optional milling functions. The correct choice starts with the machine’s process and interface, not a generic description such as “three-axis CNC.”
Identify the Lathe Workflow
Start by defining the work the machine performs. A turning machine commonly uses X and Z as its principal motion axes, while a machine with additional functions may need a different configuration. Record the workpiece type, the normal turning sequence, any engraving or milling operation, and the operator controls that must remain available.
This is important because a controller designed for a router, a rotary carving machine or a plasma table can share an axis count without sharing the same motion workflow or machine signals.
Check the Machine Interface
For a new build, list the controlled axes, drive type, input and output requirements, spindle-related functions and operator interface needs. The A132 product information includes definable I/O and customizable operation interfaces for machine-builder requirements; specify the required functions rather than assuming a default cabinet layout.
For a replacement, photograph the installed controller, interface board, terminal labels, drive connections and wiring before removal. Retain any available parameter information. The controller label alone is not enough to establish that another platform can be connected directly.
Choose by Function, Not by Family Name
The A132 is a strong candidate when the machine is a turning or engraving lathe and its X/Z workflow, interface and auxiliary functions align with the intended configuration. It is not the default choice for a standard three-axis router, ATC router or plasma machine. If the machine needs a fourth axis, define its actual role before comparing a different controller category.
Information to Send Before Ordering
Provide the machine type, the current controller model, the number and purpose of controlled axes, drive and spindle details, required I/O, interface-board photographs and cabinet wiring. This gives CINKR the information needed to assess the practical A132 configuration before quotation.