


BEST FIT
Choose A12 if:
- The machine is built for plasma or flame cutting.
- Torch sequencing and any separate height-control device can be matched.
- The A12 interface fits the cutting machine wiring.

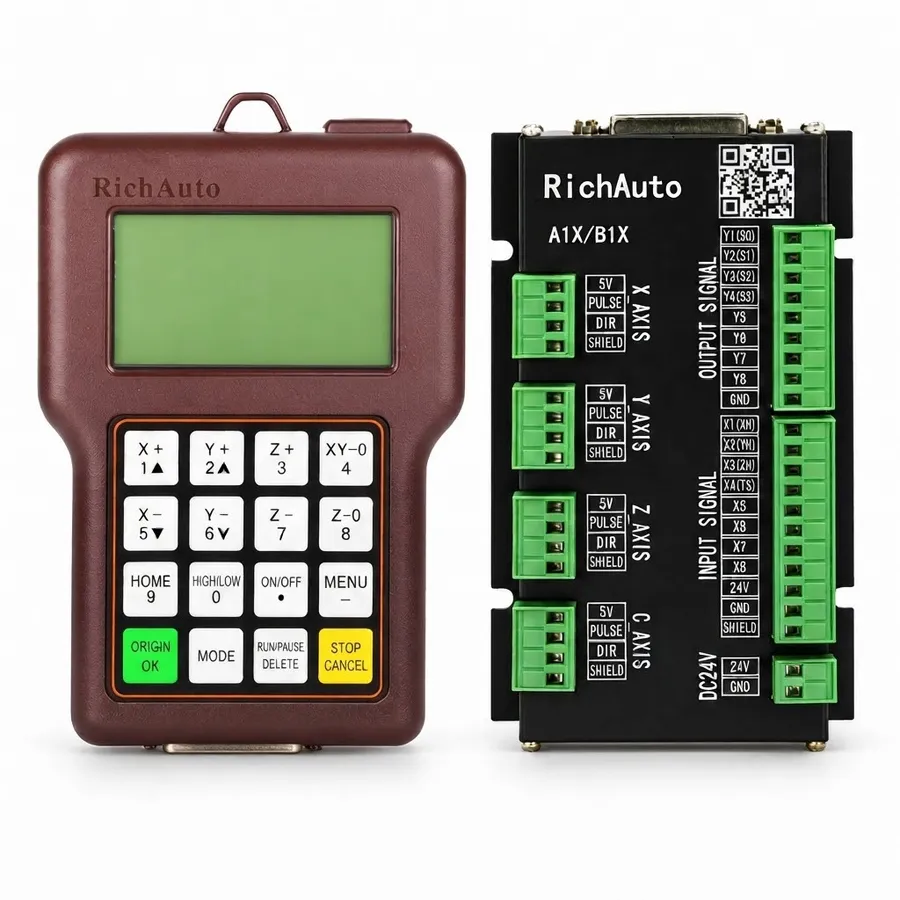
RichAuto A12 handheld controller and interface board. Reference photo; confirm the supplied controller and interface-board revision.
A1X SERIES · RA-A12
DSP control for plasma and flame-cutting applications, with torch interfaces and the electrical environment checked before integration.
Series: Browse the A1X controller range
CINKR supplies new, genuine RichAuto controllers and supports single-unit replacement orders. Eligible faults are covered by a one-year warranty. Most orders are dispatched within three working days after payment.
The supplied components, configuration, shipping cost and delivery estimate are confirmed in your quotation. Delivery, warranty and return terms.
PRODUCT GUIDE
DSP control for plasma and flame-cutting applications, with torch interfaces, arc voltage and electrical interference checked before cabinet integration.
QUICK DECISION
BEST FIT
CHECK BEFORE ORDERING
CONSIDER ANOTHER MODEL IF
The RichAuto A12 is a heavy-duty handheld DSP motion controller engineered specifically for industrial CNC plasma tables and oxy-fuel flame cutting machinery. Unlike conventional woodworking routers that experience steady mechanical cutting loads, thermal metal cutting systems operate in an electrically hostile production environment dominated by intense electromagnetic interference, high-voltage spark discharge during arc initiation, and thermal expansion across conductive metal plates.
Operating entirely as an embedded standalone architecture, the A12 executes interpolation directly on an internal high-speed digital signal processor. This eliminates the catastrophic communication dropouts, operating system crashes, and electrical ground loops that frequently plague office computer towers connected to plasma cutting equipment on factory floors. Operators command the entire cutting cycle from a rugged handheld pendant, navigating preheat dwell parameters, pierce height coordinates, and cutting speed overrides without stepping away from the cutting table. For machine manufacturers building new cutting tables or retrofit shops replacing obsolete PC controllers, request an A12 quote configured for your specific cutting torch power supply.
CNC plasma cutting machines frequently display varying model designations across manufacturer listings, including A12, A12E, A12S, and A12C. These suffix designations identify keypad language silk-screening rather than differing internal motion capabilities:
| Model Marking | Keypad Faceplate Language |
|---|---|
| A12 | Base plasma and flame controller platform |
| A12E | English-only keypad faceplate (Export standard) |
| A12S | Bilingual (Chinese + English) keypad faceplate |
| A12C | Bilingual (Chinese + English) keypad faceplate |
All plasma cutting logic, torch height control interfaces, high-voltage optical isolation, and firmware features are identical across A12, A12E, A12S, and A12C. The only difference is the button faceplate language. Operators can also switch menu languages directly in firmware settings. When replacing a unit, confirm your machine requirements, then submit an A12 equipment inquiry.
Each standard RichAuto A12 plasma and flame cutting kit includes the industrial hardware elements necessary for electrical enclosure integration:
Examine the grounding pigtail conductor integrated into the 50-pin cable harness during assembly. Securing this shield termination directly to cabinet earth ground is mandatory for maintaining arc transfer noise protection.
Maintaining an exact distance between the plasma torch nozzle and the steel plate is critical for edge squareness, slag prevention, and consumable longevity. Warped hot-rolled plate or thin sheet metal naturally distorts during intense thermal cutting, requiring dynamic vertical compensation. The RichAuto A12 coordinates torch elevation through dedicated interface signals:
Never connect raw plasma arc voltages directly to the A12 terminal board. All arc voltage sampling must occur through external division circuits rated for industrial isolation.
Cabinet wiring for the A12 terminates at the dedicated plasma interface breakout card mounted on the enclosure DIN rail. Terminals are isolated into discrete functional groups:
| Terminal Group | Terminal Identifier | Connected Field Signal | Electrical Characteristic |
|---|---|---|---|
| Main DC Power | 24V+, GND | Primary board DC logic supply | 24V DC regulated, 2A isolated supply |
| Torch Start Relay | Torch On / Arc Start | Triggers plasma pilot arc or flame valve | Dry contact relay closure or sinking output |
| Arc Feedback Input | Arc OK / Transfer | Cutting arc transfer confirmation | 24V optically isolated digital input |
| THC Height Signals | THC UP, THC DOWN | Directional elevation commands from THC | Active-low optically isolated inputs |
| IHS Touch Sensing | Ohmic / Plate Sensor | Workpiece top surface detection switch | Isolated 24V digital proximity input |
| Corner Speed Output | Kerf Inhibit / Corner | Height freeze during corner deceleration | Sinking transistor open-collector output |
| Drive Command Pulses | X-PUL, Y-PUL, Z-PUL | Step command outputs to axis drives | High-speed common-anode optical isolators |
| Drive Direction Lines | X-DIR, Y-DIR, Z-DIR | Direction command outputs to axis drives | High-speed common-anode optical isolators |
Ensure that field limit switches and inductive proximity sensors share the common 24V auxiliary ground without bridging into high-voltage plasma return paths.
Engineering documentation identifies two distinct wiring variants across the A12 family:
Examine the silkscreen markings on your existing breakout card before rewiring field connections. Matching board revisions avoids operational timing variances during torch firing cycles.
CNC plasma tables generate severe electrical transients capable of causing false limit trips or communication resets if shielding rules are neglected:
Following these practices ensures uninterrupted cutting execution even on high-frequency pilot arc starting machines. To discuss specific cable shielding layouts or auxiliary relay isolation, submit your electrical cabinet details for review.
When the A12 detects abnormal operating states or interrupted cutting arcs, specific diagnostic alerts appear on the handheld screen:
| Screen Diagnostic | Underlying Machine Condition | Systematic Troubleshooting Steps |
|---|---|---|
| Arc Broken / Cut Abort | Plasma arc extinguished during active motion | Check workpiece ground clamp; inspect torch nozzle and electrode wear |
| No Arc OK Signal | Torch fired but transfer confirmation not received | Verify pilot arc ignition; check plasma output relay wiring to Arc OK terminals |
| THC Limit Warning | Torch reached upper or lower physical lifter travel | Inspect plate warpage; adjust initial torch standoff distance |
| Initial Height Error | Ohmic clip failed to detect plate surface or stuck closed | Clean slag from ohmic sensing cup; inspect floating head limit switch |
| Travel Overrun Limit | Gantry or torch lifter contacted physical overtravel switch | Jog torch manually away from sensor; verify soft limit parameter entries |
Resolving torch consumable wear and grounding integrity at the source eliminates the majority of automated cut abort conditions on production plasma tables.
When ordering a replacement A12 controller for an operating plasma table or retrofitting an older thermal machine:
Submit your cutting system specifications through our A12 quotation desk to receive a verified hardware proposal.
SELECTION CHECKLIST
SPECIFICATIONS
Compare the current A1X platform below. For an existing machine, match the controller label, interface board and software version; reference documents and photos may show earlier hardware.
| Product model | A12 |
|---|---|
| Series | A1X |
| CPU | DSP |
| Internal memory | 512 MB |
| Display | 3-inch |
| Communication | USB flash drive / USB cable — Match the supplied hardware and software version. |
| Controlled axes | 3 axes |
| Control signal | Common-anode |
| Drive system | Stepper / Servo — Match the supplied hardware and software version. |
| Inputs | 8 inputs |
| Outputs | 8 outputs |
| Additional I/O | Confirm the board variant and available terminals for additional I/O. |
| Minimum input unit | 0.001 mm |
| Max. pulse frequency | 1 MHz |
| Power supply | 24V DC — Interface-board input; check its rating separately from the handle supply. |
| Interpolation | Line / Arc / Curve — Match the supplied hardware and software version. |
| Breakpoint resume | Supported — Match the supplied hardware and software version. |
| Power-failure recovery | Supported — Match the supplied hardware and software version. |
| Soft / hard limit | Supported — Match the supplied hardware and software version. |
| Password protection | Supported — Match the supplied hardware and software version. |
| Rotary axis | Not supported |
| ATC support | Not supported |
| Multi-spindle / cylinders | Not supported |
| Plasma control | Supported |
| Handwheel / MPG | Not supported — Match the supplied hardware and software version. |
| Network communication | Not supported — Match the supplied hardware and software version. |
COMPARE RELATED CONTROLLERS
A12 serves plasma and flame-cutting machines. Router, ATC and rotary controllers are not equivalent alternatives; match the cutting sequence and machine interface.
| Model | Main use | Axes | Display | I/O | Relationship |
|---|---|---|---|---|---|
| A12 | Plasma and flame cutting | Confirm configuration | 3-inch | 8 inputs / 8 outputs | Selected model |
A12 alternatives depend on the required motion and machine functions. A related model is not a promise of interchangeable wiring or firmware.
DOWNLOADS
Download reference documents below. Match the controller and interface-board revision before using any wiring instructions. For a replacement or new order, request the documents for the exact supplied hardware from CINKR.
Reference wiring diagrams with English labels and signal notation. Confirm the matching board revision before using them.
Free direct downloadReference instructions and parameter guidance, mainly in English with some Chinese labels. These reference editions may describe earlier hardware; the supplied unit must match the document.
Free direct downloadFAQ
The A12 motion system incorporates specialized firmware algorithms and input isolation specifically designed for thermal metal cutting. It features dedicated logic for pierce delays, torch ignition outputs, arc-voltage feedback monitoring, and torch height controller (THC) coordination, alongside hardened noise immunity against high-frequency arc start interference.
No. The A12 breakout board interfaces with an external standalone torch height controller (THC) or an external arc voltage divider supplied with your plasma power source. The A12 receives digital arc transfer confirmation and directional up/down height commands rather than raw 300V arc voltages directly.
Documentation identifies standard A12 and A12-2AXIS-delay wiring variants. The delay variant provides dedicated hardware timing logic for pierce dwell delays and pneumatic torch lifter sequencing required on heavy plate cutting systems.
Yes. The A12 software includes parameters for preheat timing, cutting oxygen solenoid control, and ignition sequences tailored for oxy-fuel gas cutting torches.
Specify the plasma power source model, torch height control interface signals, cabinet auxiliary DC voltage, and motor drive types. Submit photos of existing terminal blocks through our quote form.
No. The A12E (English keypad) and A12S/A12C (bilingual keypad) feature identical Arc OK transfer inputs, THC up/down directional channels, and torch ignition relay outputs.
Yes. A12S and A12C units feature dual-language firmware allowing operators to toggle the on-screen display language to English in the system settings menu, although keypad buttons retain bilingual silkscreens.
Record the plasma power source model, pilot arc starting mechanism, standalone THC model, and submit photographs of the breakout board terminal connections.
REQUEST A QUOTE
Tell us the quantity and destination country. For a replacement or upgrade, include any available machine details below. This form only prepares your message; nothing is submitted or stored.